
Line
Farm stall and micro
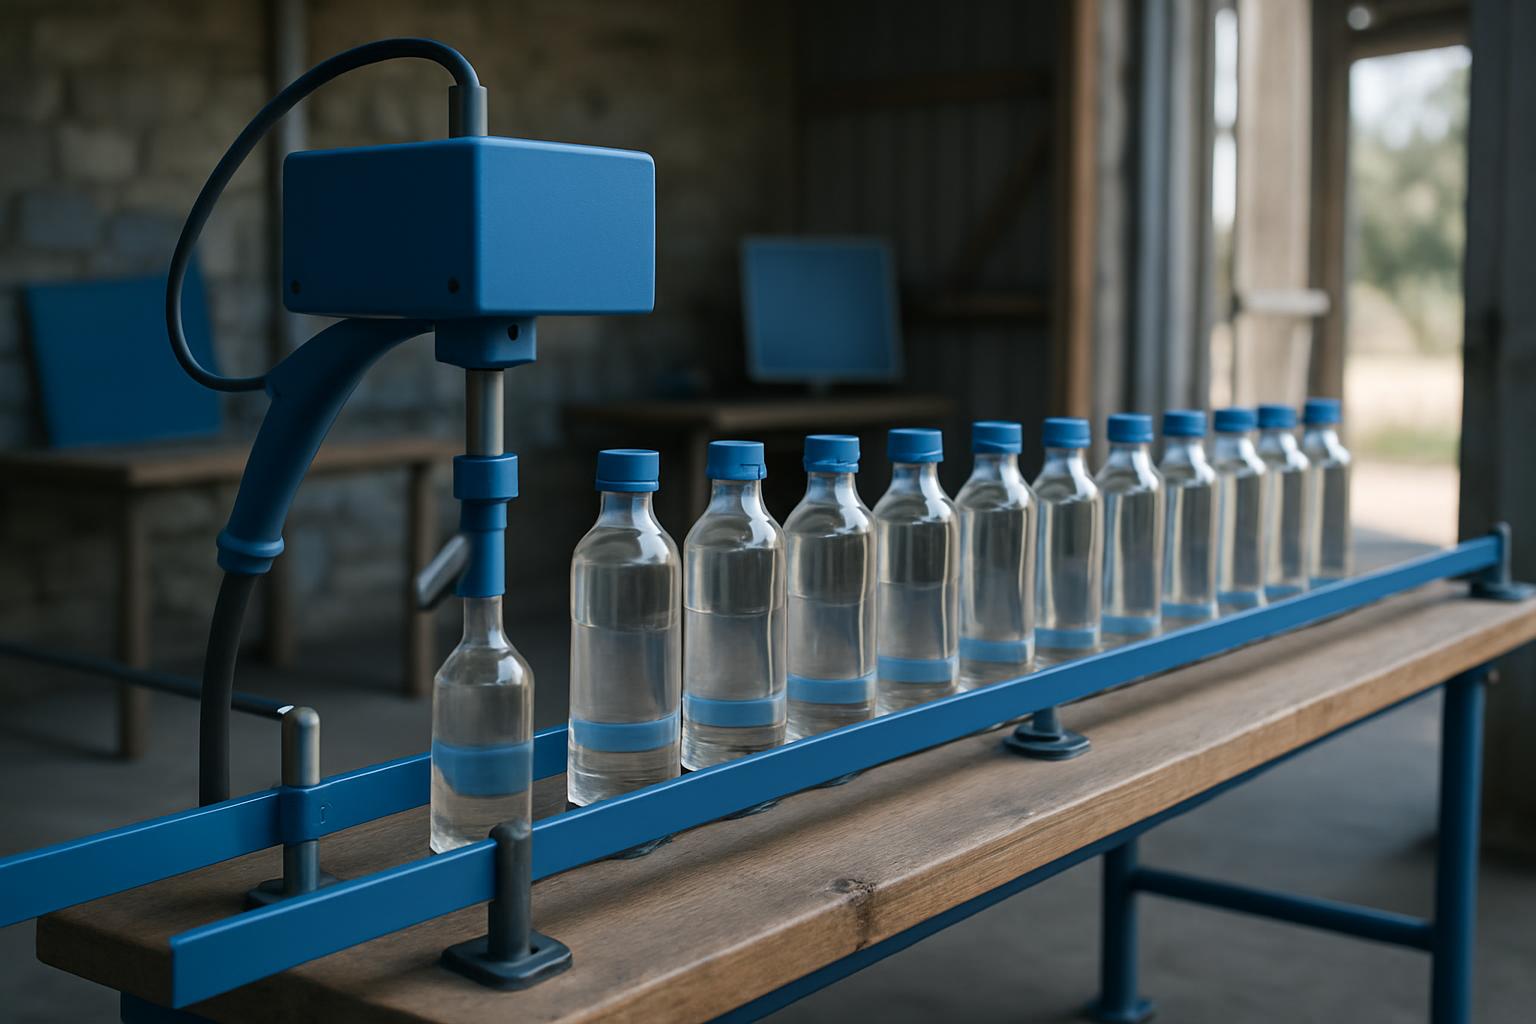
Farm stalls and micro-breweries sealing small batches with a portable wand.
Farm stall and micro
Farm stall bottling in South Africa is mixed work: chilli sauce, chutney, dressing, cordial concentrate, vinegar blends and brewery trial bottles often share one filling table. Packs are mostly PET or HDPE with lined screw caps, and the fill can be warm, sticky, oily or foamy. The seal plan starts at the cap: the liner must lie square against the bottle mouth with no sauce, oil or syrup on the contact area.
The usual call comes after a market batch has wept in a crate, or when a retailer asks for a tamper-evident inner seal on a short run. Farm stall rooms often have a filler, hand capper, wipe-down space and case packing area in one bay. That layout suits a hand wand cell when cap torque, rim cleanliness and cooling time are controlled.
Packs, closures and fill conditions
Bottle fit is checked from the neck finish, not from the label artwork. A 28 mm sauce cap, a 38 mm syrup cap and a 45 mm condiment cap need liners cut to the correct outside diameter and matched to the bottle material. The Foil & Die Kit is used to cut trial liners for the sauce, cordial and sample bottle necks common in farm stall packing.
Warm chutney and thick sauce can leave product on the land when the nozzle strings. Oils creep up threads if the operator overfills. Brewery samples foam into the cap if capped too soon after filling. Each condition gives the liner a poor contact patch. The floor fix is repeatable fill level, a clean land where needed, square capping and a recorded setting for that bottle.
Recommended hand-seal cell
For low-volume market batches, the Manual Hand Sealer is commonly set up with a wand stand, cap samples and a short setting sheet for each product. The operator fills, checks the rim, caps, places the bottle under the wand, runs the timed cycle, then moves it to a cooling area. For longer retail batches, Seal Induction Compact gives a benchtop timed sealing station for up to 25 bpm.
A clean bench sequence removes most batch arguments: fill, wipe the land if product has climbed the thread, cap to the chosen torque, seal, cool, open a sample for bond check, invert batch samples, label dry bottles and pack into cases. Case packing stays last because warm seals need handling time, and wet bottles can scuff labels or soften cartons.
Seal failures and maintenance
Half-moon seals come from a tilted cap, a liner shifted inside the cap, or an oval bottle neck after hot product has stressed thin plastic. Scorched rings come from too much heat time for the bottle wall and liner stack. Loose foils usually trace back to light cap torque, an oily land or damp cap storage. Pinholes and weeping at the thread often show product trapped on the rim.
Maintenance is small but firm. Keep the wand face clean and dry, keep the cable clear of hot pots and carton knives, and keep lined caps in closed bags or tubs between batches. Check hand cappers for worn pads, because torque drift changes the seal result even when the sealer setting has not moved. After a power cut, run trial bottles before returning sale stock to the bench.
Typical customer situation
A Worcester farm stall packing chilli sauce and cordial concentrate needed a portable seal method that one operator could use between cooking and Saturday market packing. They brought PET bottles, three cap sizes and lined closures to Meadowdale Industrial, Germiston. The trial matched wad sizes to each closure, set a separate hand-wand time for each pack, and gave the operator a simple reject rule for bottles with sauce or syrup on the mouth before sealing. The same notes then became the Saturday packing sheet, so relief staff could run the chutney, cordial and brewery sample bottles without guessing the timer setting.
What our Bottle Sealing customers say
Verified Google reviews
