
Resource
Coil gap guide
How the gap between induction head and cap top changes foil heating on PET and HDPE lines.
Coil gap guide
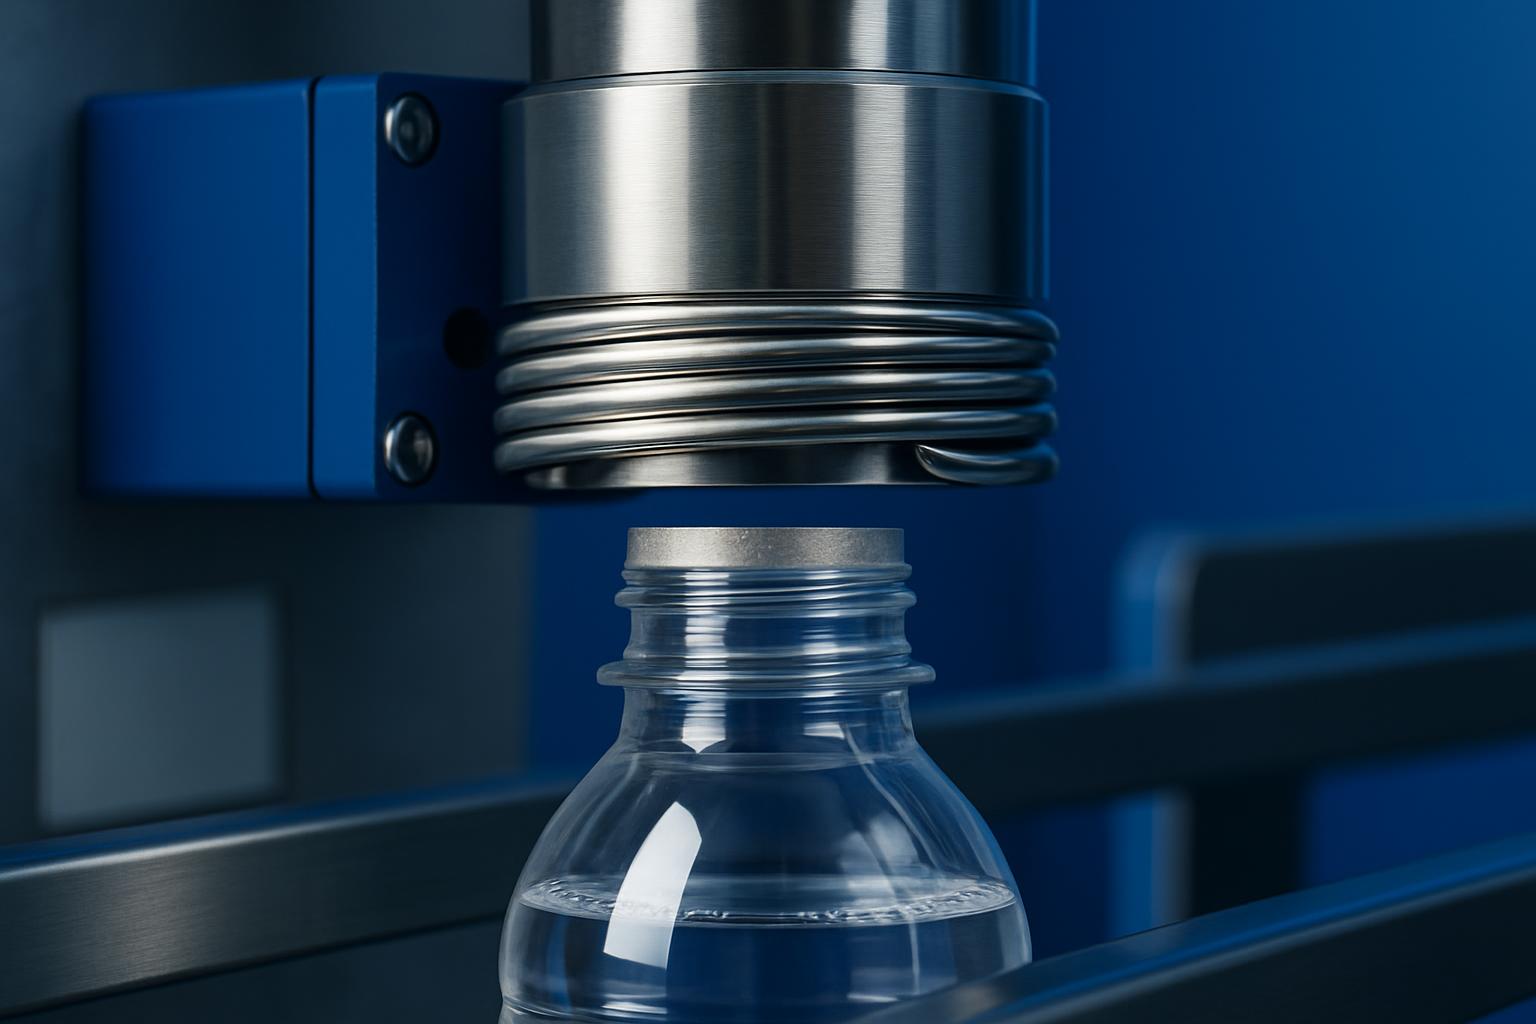
Coil gap is the measured space from the induction head face to the top of a closed cap. Setters, maintenance leads and QA staff check it when a new SKU starts, when a cap or liner lot changes, after head-height work, and whenever peel tests move from clean bond to scorched foil or loose patches.
The head carries alternating current, which creates a magnetic field that reaches the aluminium foil liner and heats it. A smaller gap heats faster, while a wider gap heats slower. The head stays above the cap, with no touching, pressing or clamping. Cap torque holds the liner on the bottle land while plastic caps and PET or HDPE bottles let the field pass.
Fill in the guide in order
Start with the SKU name, bottle resin, measured neck finish, cap reference and liner construction. Record the sealer used: Seal Induction Pro on a continuous PET or HDPE line, or the benchtop Seal Induction Compact during lab checks, trial batches and short-run contract packing. Seal Induction Compact is benchtop, up to 25 bpm.
Next record cap torque, starting gap, power setting, belt speed and sample count. Run bottles at the planned line pace, cool them long enough for a fair peel, then open and record the land print. Move either height, power or speed for the next pull, not all together, so the guide line shows cause and result, not a mixed adjustment.
Worked entry from a line trial
A filled-in entry could read: 500 ml rectangular HDPE cleaner pack, 38 mm cap, pulp-backed induction liner, torque taken from the current torque recipe, Seal Induction Pro over the conveyor. First run shows a dull bond on the shoulder side and foil lifting at one arc of the land.
The setter lowers the head by one indexed movement, keeps power and belt speed fixed, then runs the next counted sample. The second peel shows a full land print with no brown scorching, no melted cap skirt and no loose crescent near the thread start. The final guide entry names the cap lot, liner lot and accepted head-height index.
Read the failure marks
Too little gap scorches the liner. Look for brown foil marks, burnt smell, wrinkled heat-seal layer or heat stress near the PET neck finish. Raise the head in one controlled movement, keep other settings unchanged, then repeat the sample. If the cap is loose, correct torque first, because induction heat cannot replace liner contact.
Too much gap creates cold, unbonded patches. The foil may lift from the land in one piece, bond on one side only, or show a leak path where the liner never reached bonding temperature. Bring the head closer or adjust power as a separate trial. A height-indexed coil mount gives repeatable settings during cap-height changeovers.
Common mistakes to avoid
The common errors are measuring to the shoulder instead of the cap top, changing power and height together, using bottles capped at uneven torque, and copying a setting from a different cap height. Treat PET and HDPE entries separately when cap top thickness or liner build changes, even where the neck finish looks similar.
Keep the head face clean, the height slide tight and the guides set so each cap runs through the same centre under the coil. If results drift during one shift, check bracket movement, conveyor tracking, capper variation and bottle rock. For new liners, send the cap drawing, liner stack and three trial readings from this coil-gap sheet through our contact form.
