
Stellenbosch
Stellenbosch RTD bands
Neck bands surviving cooler condensation for RTD launches.
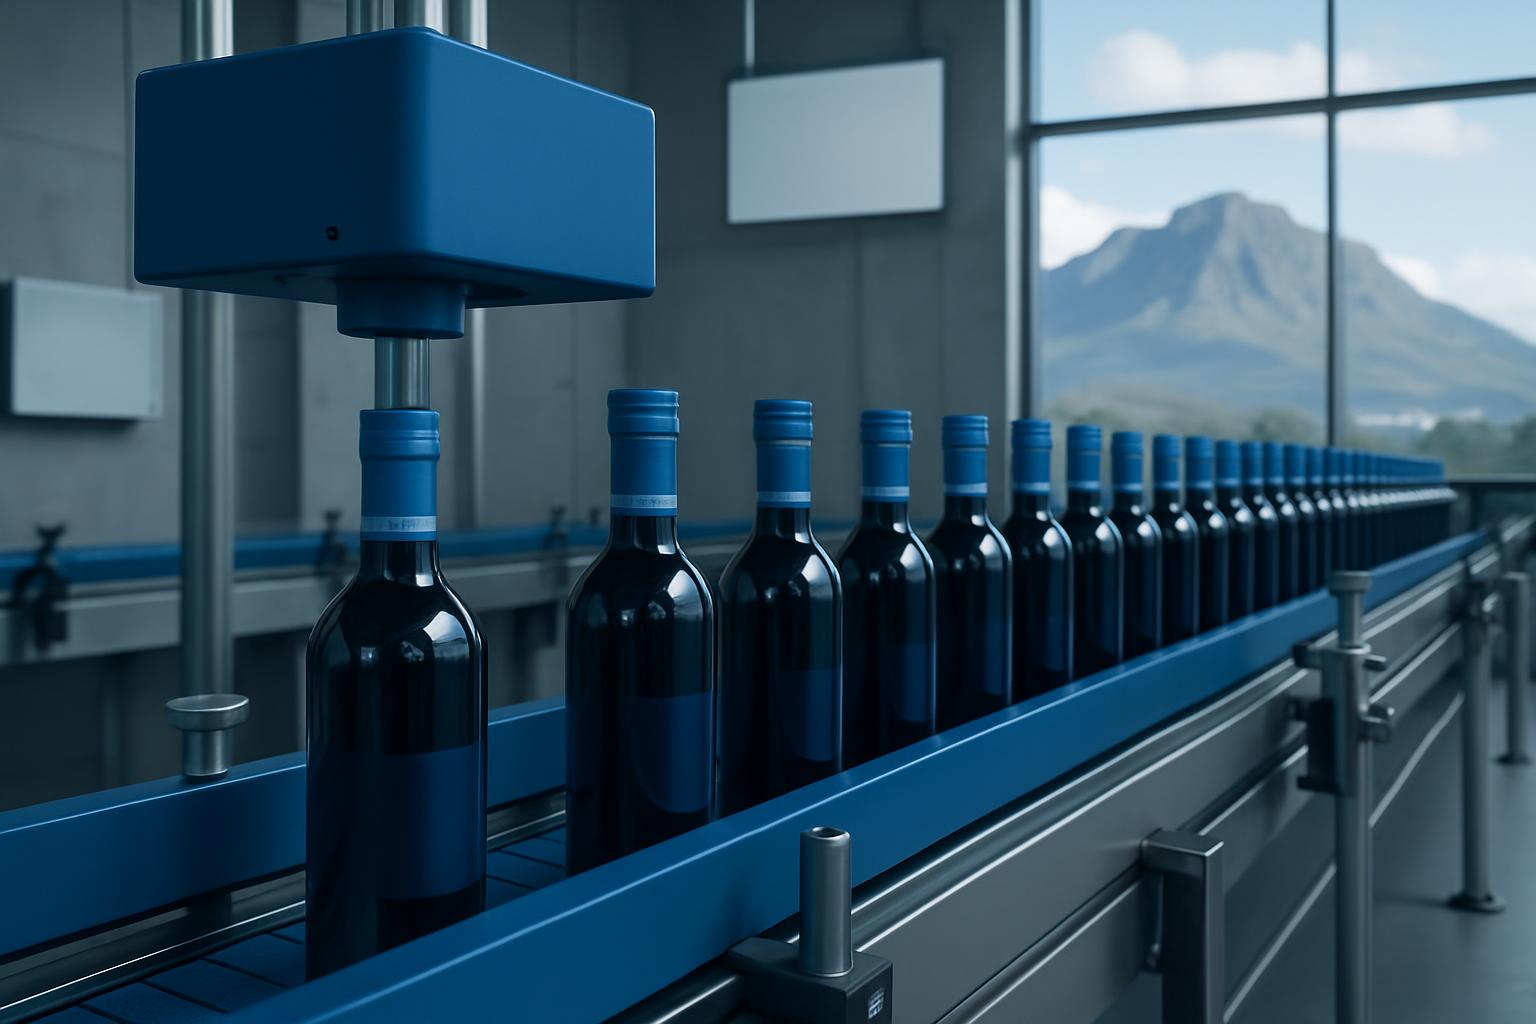
Stellenbosch RTD bands
A Stellenbosch wine RTD launch needed tamper bands that stayed tight after cold storage, chilled transport and retail fridge handling. The bottles carried 28 mm and 33 mm neck finishes, so the band programme had to cover two cap sizes without wrinkles, lifted skirts or blocked tear starts. The plant chose a Band Shrink 120 cell for the single-lane RTD run.
The job started when neck bands lifted after the packs warmed and cooled again. Moist caps made the symptom worse, especially where condensation collected under the band edge. The brief was floor-level: hold bottle pitch, set sleeve height from the cap shoulder, place the tear perforation where shoppers could find it, and dry the neck area for downstream handling.
Survey and set-up sequence
The site survey followed bottles from cap exit to sleeve application and through the steam section. Marnus Esterhuizen checked straight conveyor space, side guide position, steam supply, drain fall, sleeve storage at the operator side and cleaning access. The RTD bottles were light enough to move during steam contact, so rail pressure and bottle pitch were marked before heat-up.
The 28 mm finish was dialled in first, followed by the 33 mm cap once the smaller neck gave a repeatable shrink. Sleeve lay-flat was matched to cap diameter, sleeve height was checked against the tamper band artwork, and the tear perforation was turned to the agreed operator-facing position. The sleeve feed tray was set so each band entered square.
Commissioning fault and fix
During the first production weeks a fault showed as a lifted lower edge on cold bottles pulled from storage. The band looked tight when it left steam, then crept upwards after condensation formed around the cap skirt. The team slowed the line, checked sleeve height with sample bottles, and compared dry caps against wet caps at the same steam pressure and dwell.
The cause was traced to two linked settings: sleeve height sat too high on the taller cap, and condensate was dripping back near the exit. The fix was to drop the sleeve datum slightly, reset the tear perforation position, open the drain path and tune steam pressure so the lower band edge recovered against the neck. Notes went into the plant’s steam start guide.
How the RTD line is run now
Operators now run a short warm-up before the first saleable case. They check steam at the manifold, view bottles at the chamber entry and exit, then confirm band height, tear start and skirt grip by hand. Bottle pitch is kept even so each neck receives the same dwell. If cold-room bottles arrive sweating, the setter gives the necks time to shed surface water.
Changeover between 28 mm and 33 mm finishes is handled as a sleeve and rail job. The setter changes sleeve stock, checks lay-flat against the cap, resets guide rails and confirms the first ten bottles for height and perforation. The band sleeve size guide stays with the RTD change parts.
Care, cleaning and support
Maintenance focuses on the parts that touch steam and water. The crew wipes the chamber area, checks the steam hood seal, clears condensate paths and inspects the feed tray for burrs that can nick a sleeve. A worn hood edge can throw steam unevenly across the cap, so the gasket set is logged with RTD spares.
The plant keeps notes on steam pressure, dwell, sleeve batch, cap size and any condensation comments from the shift. Those records make repeat RTD launches quicker because faults are tied to bottle temperature and sleeve fit rather than guesswork. For the next RTD pack, the trial plan includes cold bottles, wet caps and final artwork so drying and tear perforation can be signed off together.
What our Bottle Sealing customers say
Verified Google reviews
