
2026-09-07
Vision for missing foils
What Seal Inspect Vision flags before case pack on sauce lines.
Vision for missing foils
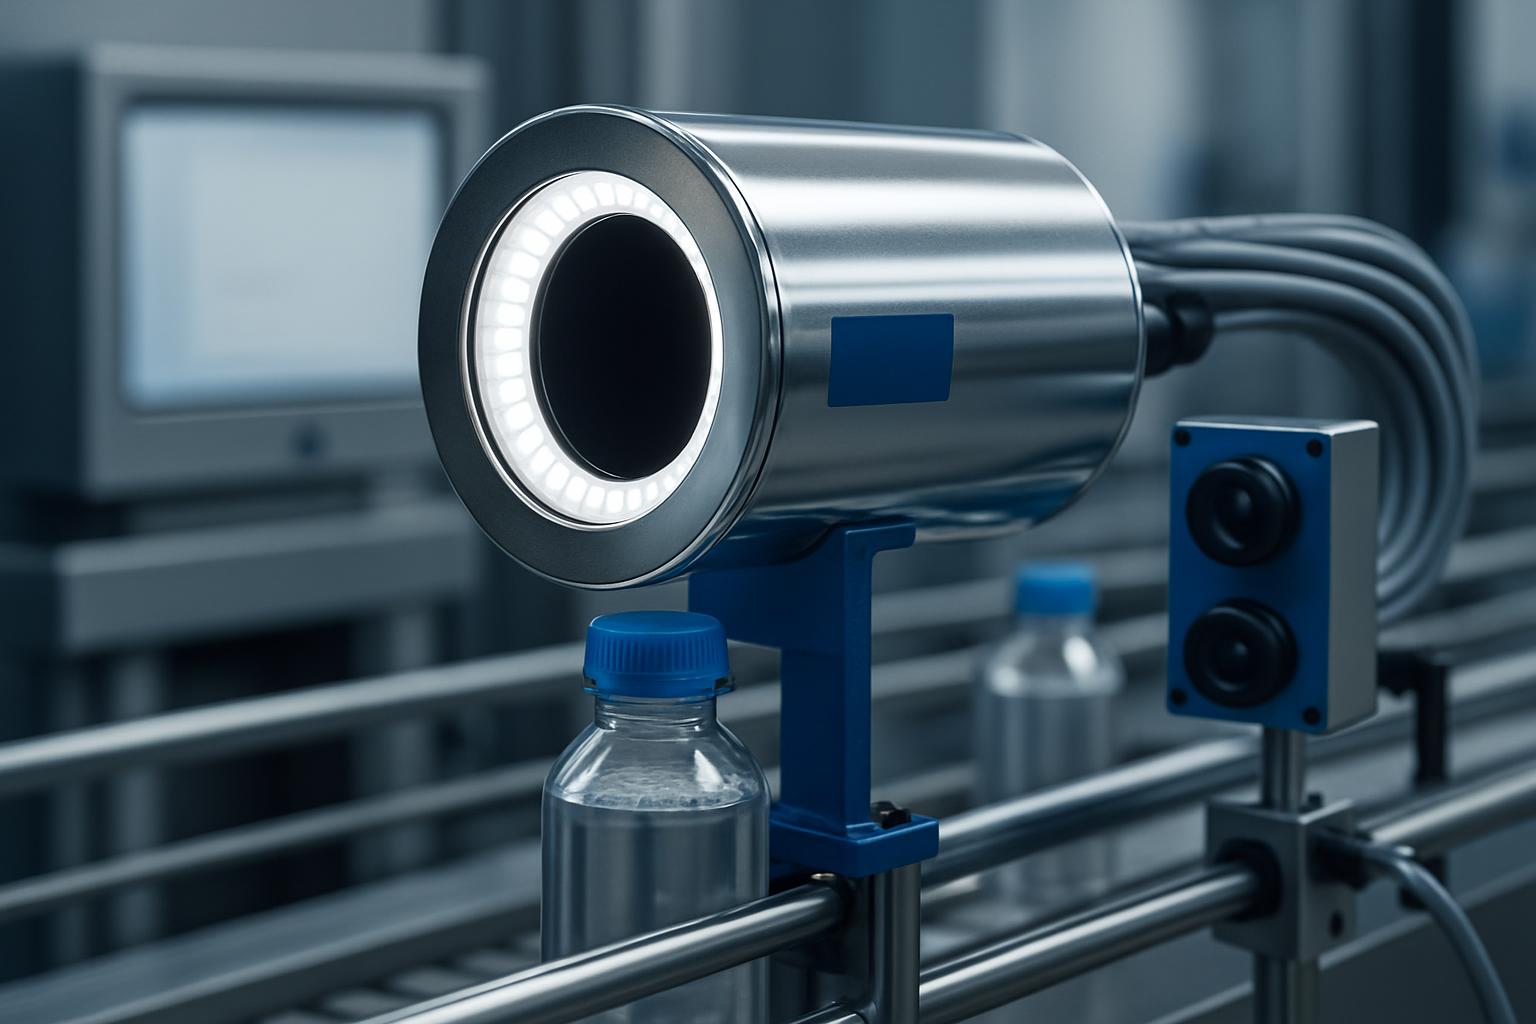
Missing foils hurt a sauce line at the carton stage: the bottle looks closed, the cap passes a quick glance, and the open mouth is found only when a retailer or export checker handles it. Seal Inspect Vision puts an LED-lit camera over the cap path and rejects bottles when the foil pattern is absent or broken.
On South African sauce floors, the cause is often changeover pressure. Fresh cap bags can carry the wrong liner, a hopper refill can mix closures, and a night-shift restart can run with yesterday’s cap colour in the vision programme. Sticky splash on the cap top changes the image, especially on chutney, peri-peri and marinade runs.
Why the foil goes missing
The camera finds the symptom; the capper and seal station usually create the fault. Low torque holds the liner too loosely on the bottle land, so the foil image can look broken after sealing. High torque can cock a cap on one side. A Cap Torque Station gives the setter a repeatable recipe when rejects rise.
Foil supply is the next check. A wad that fits one 38 mm finish may sit badly in another cap, and sauce plants often run PET and HDPE necks in the same week. During a tomato sauce to mayonnaise changeover, confirm wad diameter, board thickness and seal layer against the bottle land. The Foil & Die Kit keeps those checks tied to the neck finish.
Step-by-step method at the line
Set the vision cell with a clean, sealed reference bottle from the current SKU. Teach the cap colour, foil position and bottle pitch while the conveyor runs at production pace. Next, put three challenge bottles through: no foil in the cap, disturbed liner, and good bottle. Watch the reject pocket, then trim timing until only suspect bottles exit the main lane.
After a power dip or planned stop, run the same challenge set before releasing cartons. Confirm that the light bar is clean, the lens is dry and the guides hold the cap under the camera window without rubbing. If a cap changes from white to black, reteach the image. Wrongly taught contrast can send good bottles to reject.
Records and fit notes
Record the SKU, cap supplier batch, liner batch, torque recipe, sealer recipe, taught vision programme and reject count per run. Keep two photos for every fault type: cap top at the camera and opened pack at QA. A vision reject map turns those notes into a shift pattern, while a seal check card keeps peel tests and leak tests beside the camera data.
Fit the inspection point where the bottle has settled after sealing and where the air blast has room to move rejects clear of the main lane. A Line Integration Rail gives the camera, sensor and reject hardware a fixed mechanical reference. Wipe sauce mist from the LED cover during sanitation and check reject air after wash-down. The counter is in Meadowdale Industrial, Germiston; send a message through our contact form.
Worked example from a sauce shift
A typical 500 ml sauce line starts rejecting every few minutes after a mango atchar changeover. The operator sees each reject exit the lane, but opened packs have foil present. The record shows a switch from a white ribbed cap to a glossy black cap, with no fresh taught image. The setter cleans the LED cover, teaches a good pack, then runs the no-foil and disturbed-liner challenges. Rejects match the two challenge bottles, and QA holds the first carton until tests match the line record.
What our Bottle Sealing customers say
Verified Google reviews
